Featured OEM Systems & Commercial Vehicle Assemblies
Engineered for extreme torsional compliance, high radial loading, and zero delamination under severe commercial operating environments. Direct factory dispatch with comprehensive batch traceability.
Engineering Principles of Heavy Commercial Bushings
A technical examination into rubber-to-metal vulcanization, torsional fatigue mechanics, tribological wear prevention, and acoustic decoupling for commercial chassis stability.
Elastomeric Molecular Compounding & Damping
The operational longevity of a heavy truck suspension bushing relies predominantly on the vulcanized elastomer matrix. For high-mileage Class 8 tractors, trailers, and heavy transit buses, raw natural rubber (NR) compounded with premium carbon black (N220/N330) provides superior tensile strength (exceeding 22 MPa) and tear resistance against road debris shock loads. Chemical antiozonants and microcrystalline waxes mitigate environmental cracking under high UV radiation and extreme ambient swings (-40°C to +85°C).
Rubber-to-Metal Phosphatized Chemical Bonding
Interfacial shear failure represents the leading cause of premature field returns in commercial transport. Reliable exporters utilize an automated multi-stage pre-treatment: robotic degreasing, micro-abrasive shot blasting, zinc phosphate conversion coating, and dual-layer organosilane adhesive application (Chemlok/Megum equivalent). Thermal curing under closed hydraulic molds generates a cohesive chemical bond between outer steel sleeves and inner metal pins with peel strength far exceeding elastomer ultimate shear limits.
Torsional Elasticity & Axial Stiffness Tuning
Heavy truck torque rods, V-stays, and control arms experience compound tri-axial vector forces. The elastomeric core must simultaneously deliver high radial stiffness (to preserve steering alignment and prevent dynamic axle dog-tracking under braking torque) while preserving rotational flexibility in torsional and conical angular planes. Finite Element Analysis (FEA) guides inner profile contouring to balance load distribution across contact zones, preventing localized stress peaks that ignite fatigue tearing.
| Bushing Architecture | Material Core | Static Radial Load | Angular Misalignment | Primary Commercial Fitment | Service Life Cycle |
|---|---|---|---|---|---|
| Torque Rod Bushing (Straddle/Taper) | NBR / Natural Rubber Core | > 120 kN | ±15° Torsional / ±8° Conical | Rear Tandem Axles, V-Stay Stabilizers | 600,000+ km |
| Cabin Damper Isolator Bushing | Hydraulic / Low Durometer NR | > 25 kN | ±5° Omnidirectional | Commercial Cab Rear Suspension Mounts | 450,000+ km |
| Leaf Spring Eye Bushing | Bi-Metallic / Vulcanized Rubber | > 180 kN | ±12° Oscillating | Parabolic Multi-Leaf Front/Rear Springs | 500,000+ km |
| Anti-Roll Bar Bushing | High-Density Polyurethane (PUR) | > 85 kN | Continuous Rotary Slip | Front Axle Sway Bars, Heavy Haulage | 750,000+ km |
25+ Years of Automotive Manufacturing & Global Export Leadership
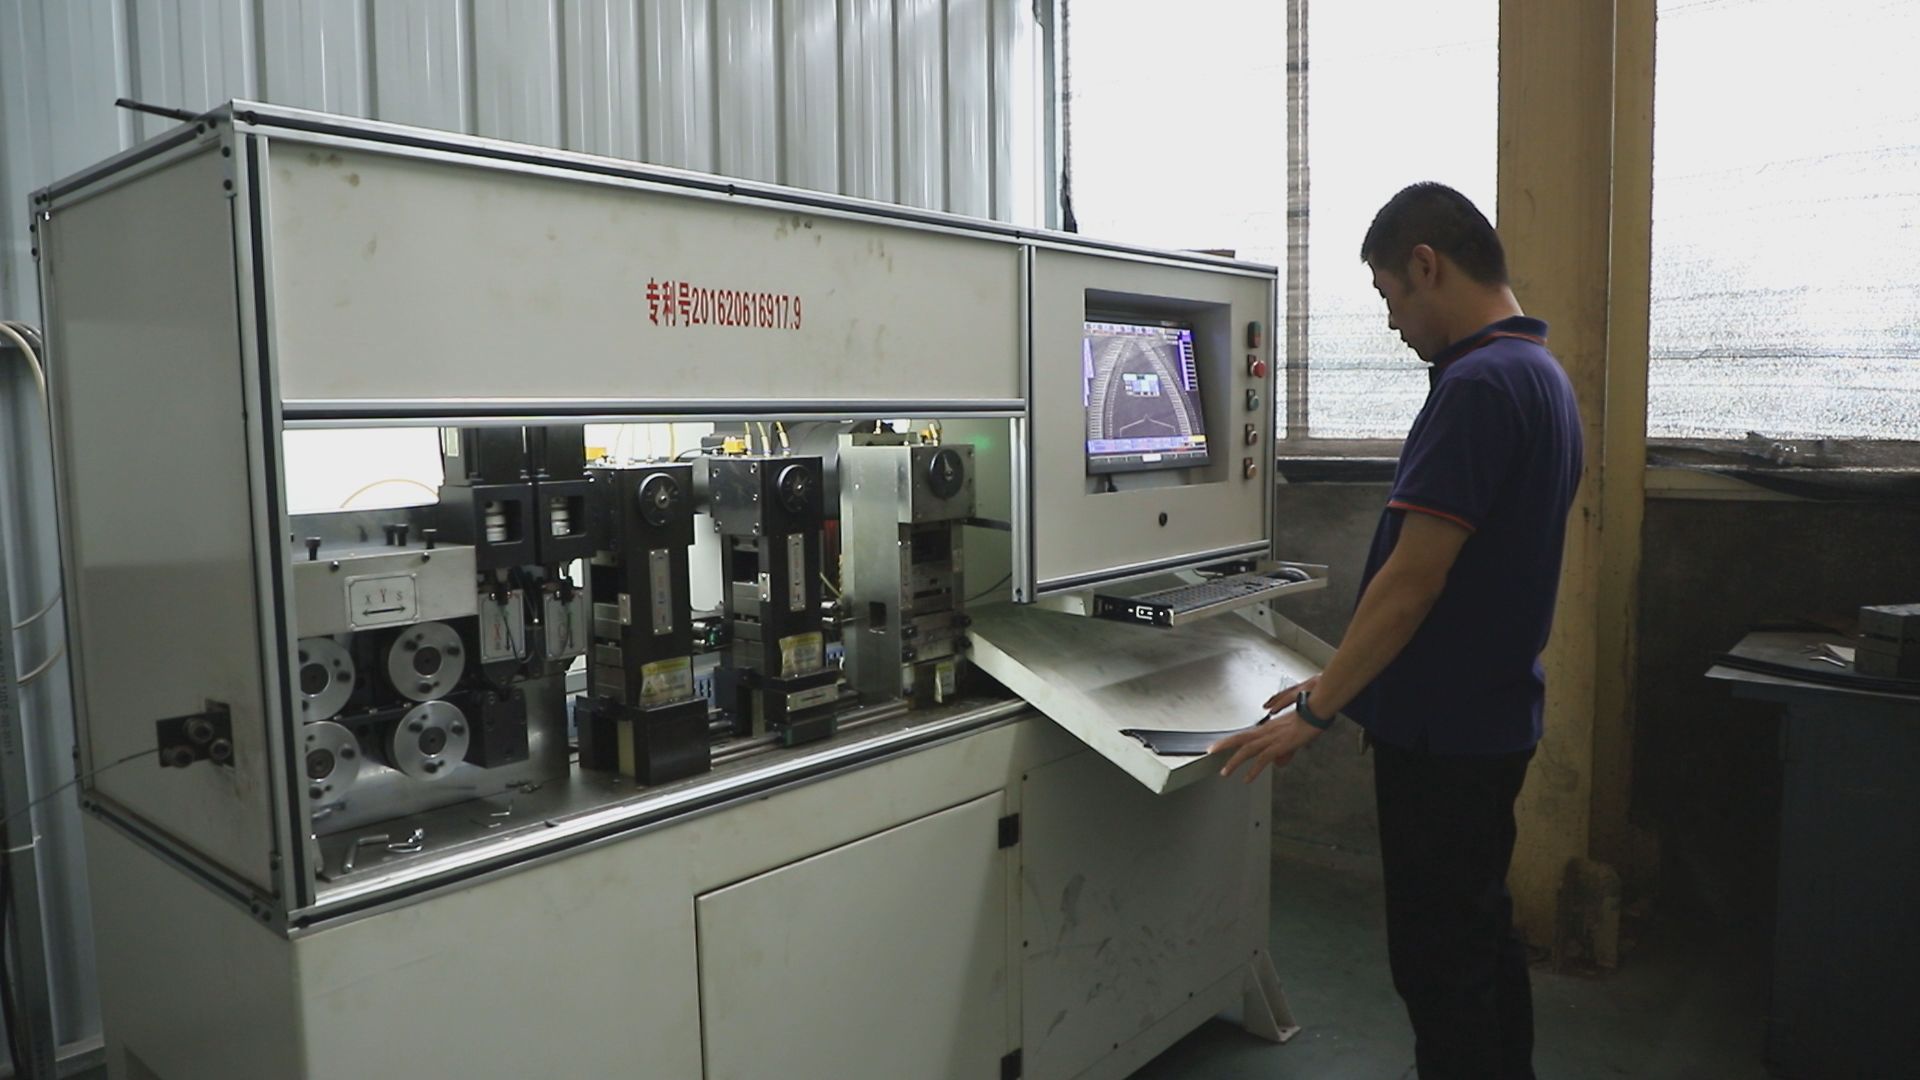
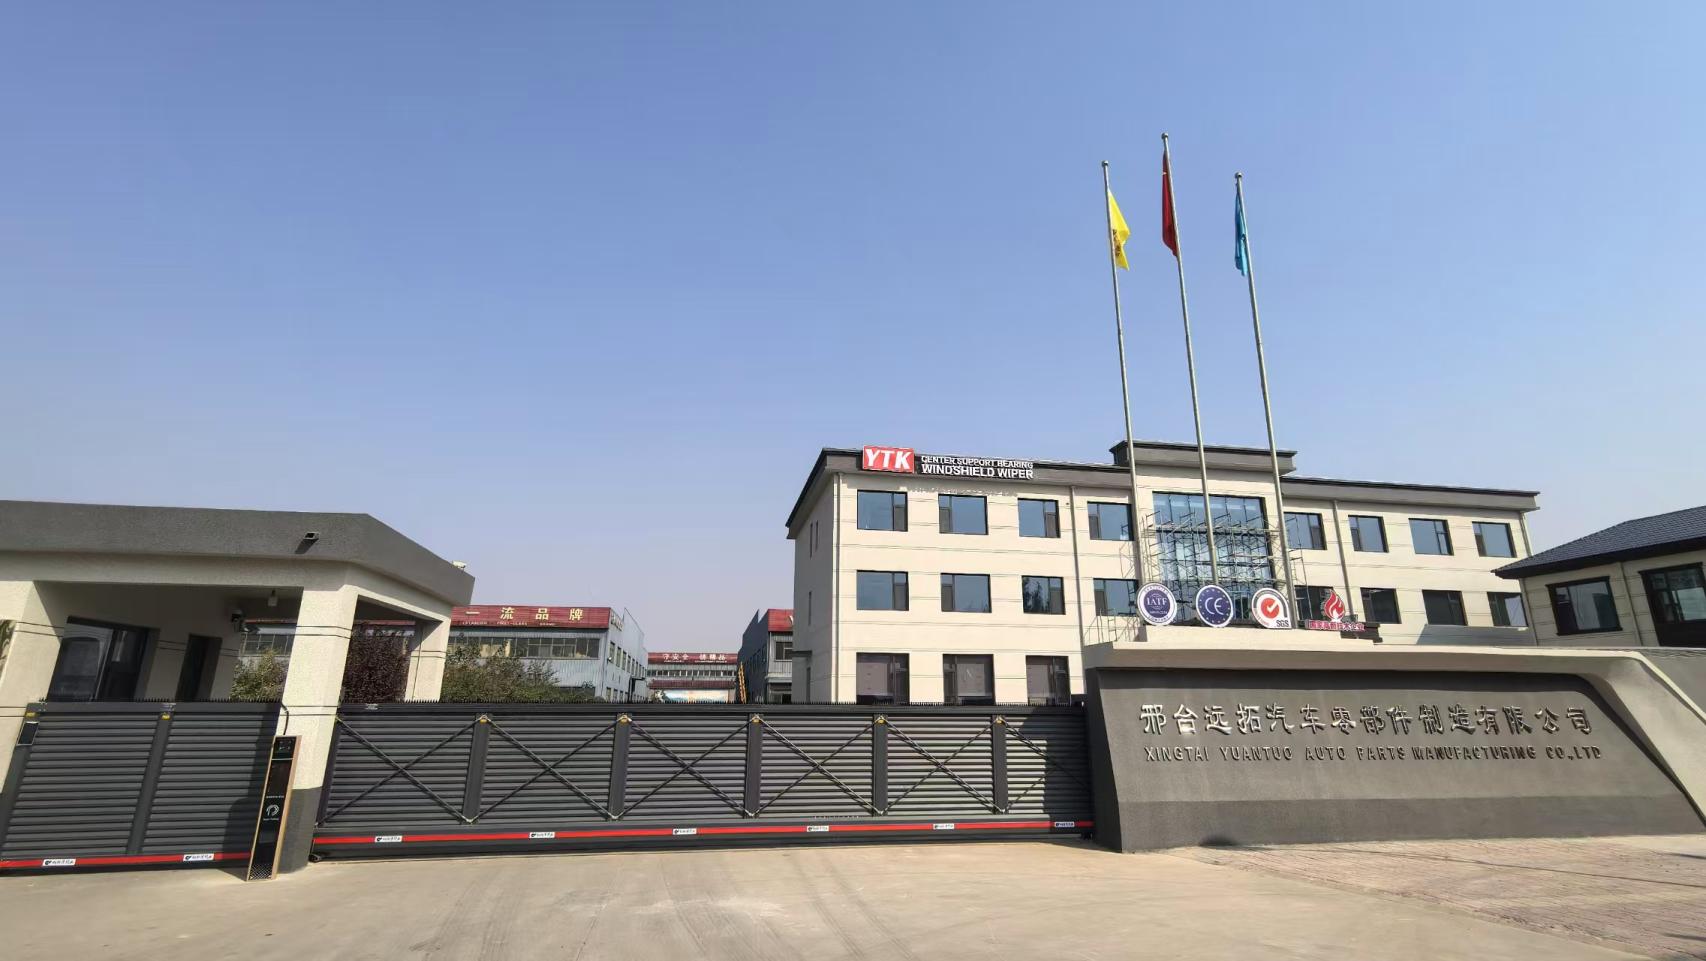
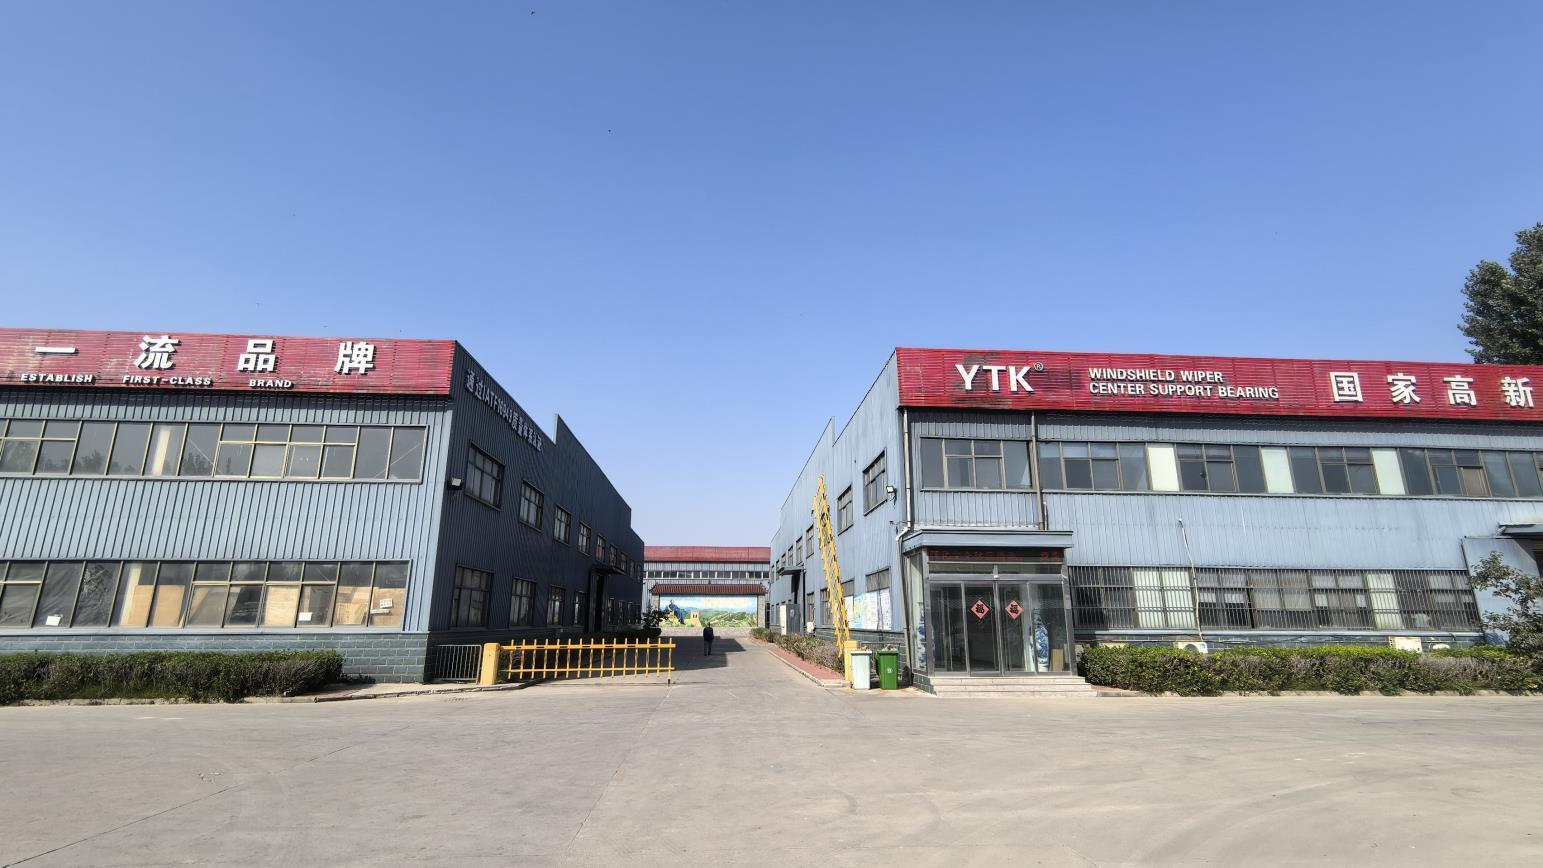
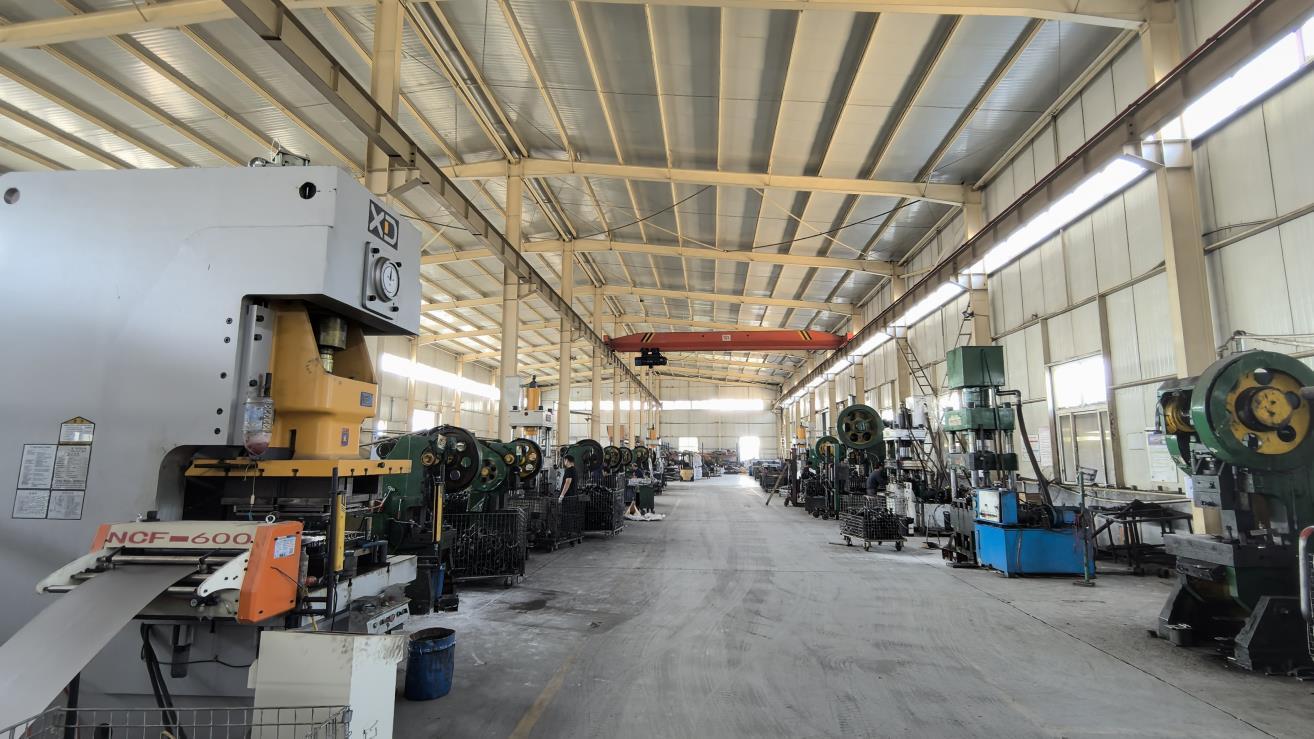
Founded in 1997 in Taojiatun Industrial Park, Xingtai, Hebei Province, Xingtai JES Auto Parts Manufactuer Co., Ltd. has grown from an authoritative mechanical damping and center support bearing specialist into a globally trusted OEM & ODM manufacturer. With a dedicated 30,000 m² modern manufacturing plant, our vertically integrated capability controls every facet from raw polymer compounding to high-precision robotic assembly.
Unlike commercial trading intermediaries, we execute direct material formulation, fatigue bench-testing, dynamic durometer calibration, and automated corrosion passivation in-house. Our operations maintain rigorous IATF 16949 automotive manufacturing management disciplines, backed by comprehensive on-site facility validation from TÜV Rheinland and international CE product compliance.
- 10+ Production Lines Under One Roof
- Complete In-House Metallurgical & Rubber Labs
- 18+ Years International B2B Export Track Record
- Private-Label Laser Marking & Custom Box Design
- Flexible Freight Execution: FOB, CFR, CIF
- Zero Defect Protocol via Computer Optical Inspection
Future Procurement Trends & Technology Evolution (2025–2030)
How fleet electrification, total cost of ownership (TCO) analytics, and green manufacturing mandates are transforming heavy commercial bushing specifications.
Electric & Hydrogen Heavy Truck Axle Weight Demands
The global deployment of Class 8 Battery Electric Trucks (BETs) and Fuel Cell Electric Vehicles (FCEVs) substantially elevates static axle tare weights due to large battery packs (often adding 2,000–3,500 kg per chassis). Furthermore, the immediate, instantaneous torque delivery of electric traction motors subjects torque rod and axle stabilizer bushings to steep torsional impact spikes. Forward-thinking procurement managers are transitioning toward dual-gradient elastomers and reinforced poly-hybrid matrices capable of handling 30% higher cyclic shear loads without increasing package envelope dimensions.
Modular SKU Rationalization & Quick-Fit Design
Commercial fleet distributors face high inventory carrying costs due to fragmented OEM cross-references across Mercedes Actros, Scania, Volvo FH, MAN TGX, Freightliner Cascadia, Kenworth, and Sinotruk platforms. The future of wholesale procurement centers on consolidated multi-fit bushing architectures that utilize precision engineered modular sleeve inserts and stepped adapter collars. This allows distributors to cover 85% of regional commercial fleets with 40% fewer unique stock keeping units (SKUs), drastically elevating stock velocity and working capital returns.
Decarbonized Vulcanization & REACH Compliance
Tier-1 commercial fleet operators in Western Europe and North America now demand environmental and chemical transparency across tier-2 and tier-3 component vendors. Traditional rubber processing formulations reliant on polycyclic aromatic hydrocarbons (PAHs), hazardous vulcanization accelerators, and nitrosamine-generating curatives are being phased out in compliance with strict EU REACH directives and corporate ESG audits. Exporters investing in clean bio-based processing oils, low-emission curing presses, and 100% recyclable metal cores gain a decisive bidding advantage.
Frequently Asked Questions for Wholesale Importers
Practical insights on technical validation, minimum order quantities, OEM customization, and container freight management.
What are the critical indicators of quality when auditing heavy truck bushing suppliers?
How do Natural Rubber (NR) bushings compare against Polyurethane (PUR) for commercial suspensions?
What are the typical Minimum Order Quantities (MOQ) and lead times for OEM private labeling?
Can your engineering team reverse-engineer bushings from OEM part numbers or physical samples?
How do you manage quality consistency across large-volume container shipments?
What trade and payment terms does Xingtai JES Auto Parts support for global distributors?
Accelerate Your Commercial Spare Parts Supply Chain
Partner directly with an on-site verified Chinese manufacturer. Request our comprehensive commercial vehicle OEM interchange cross-reference catalog and secure factory-direct wholesale pricing.
