Verified OEM & Aftermarket Fleet Portfolio
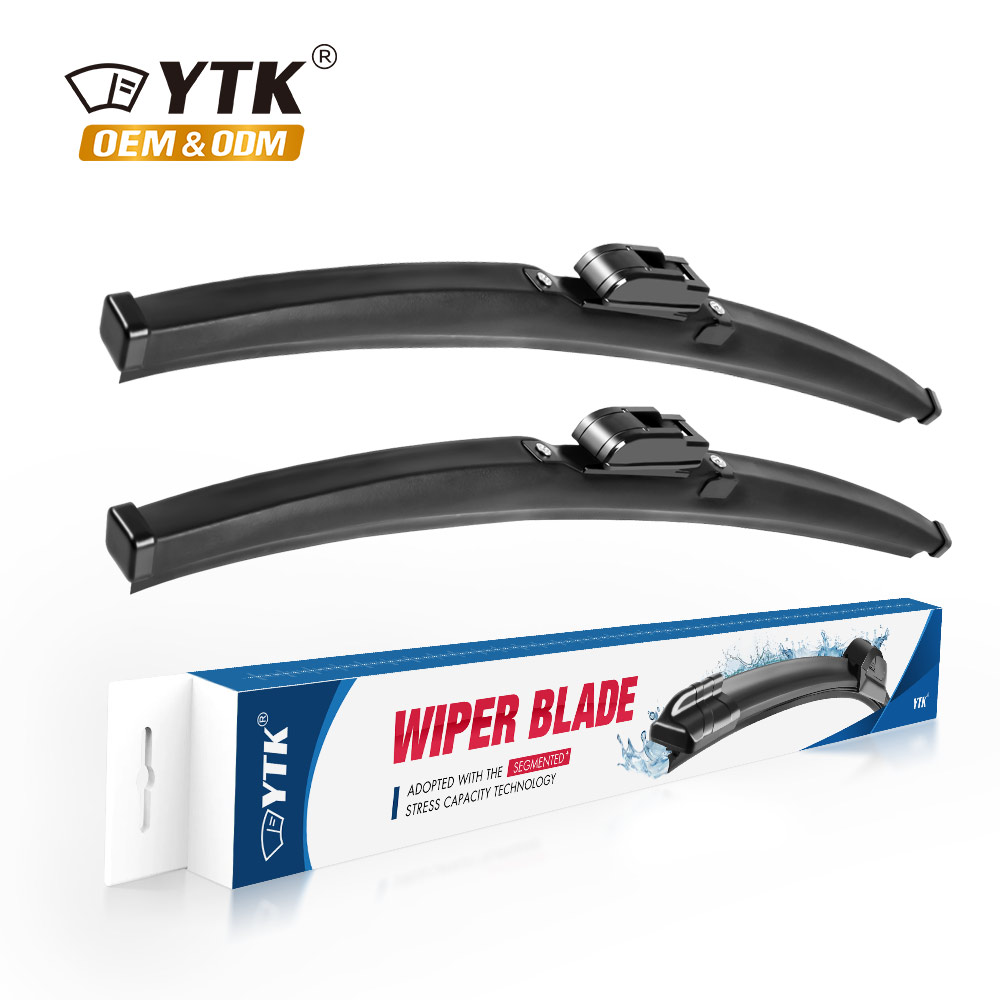
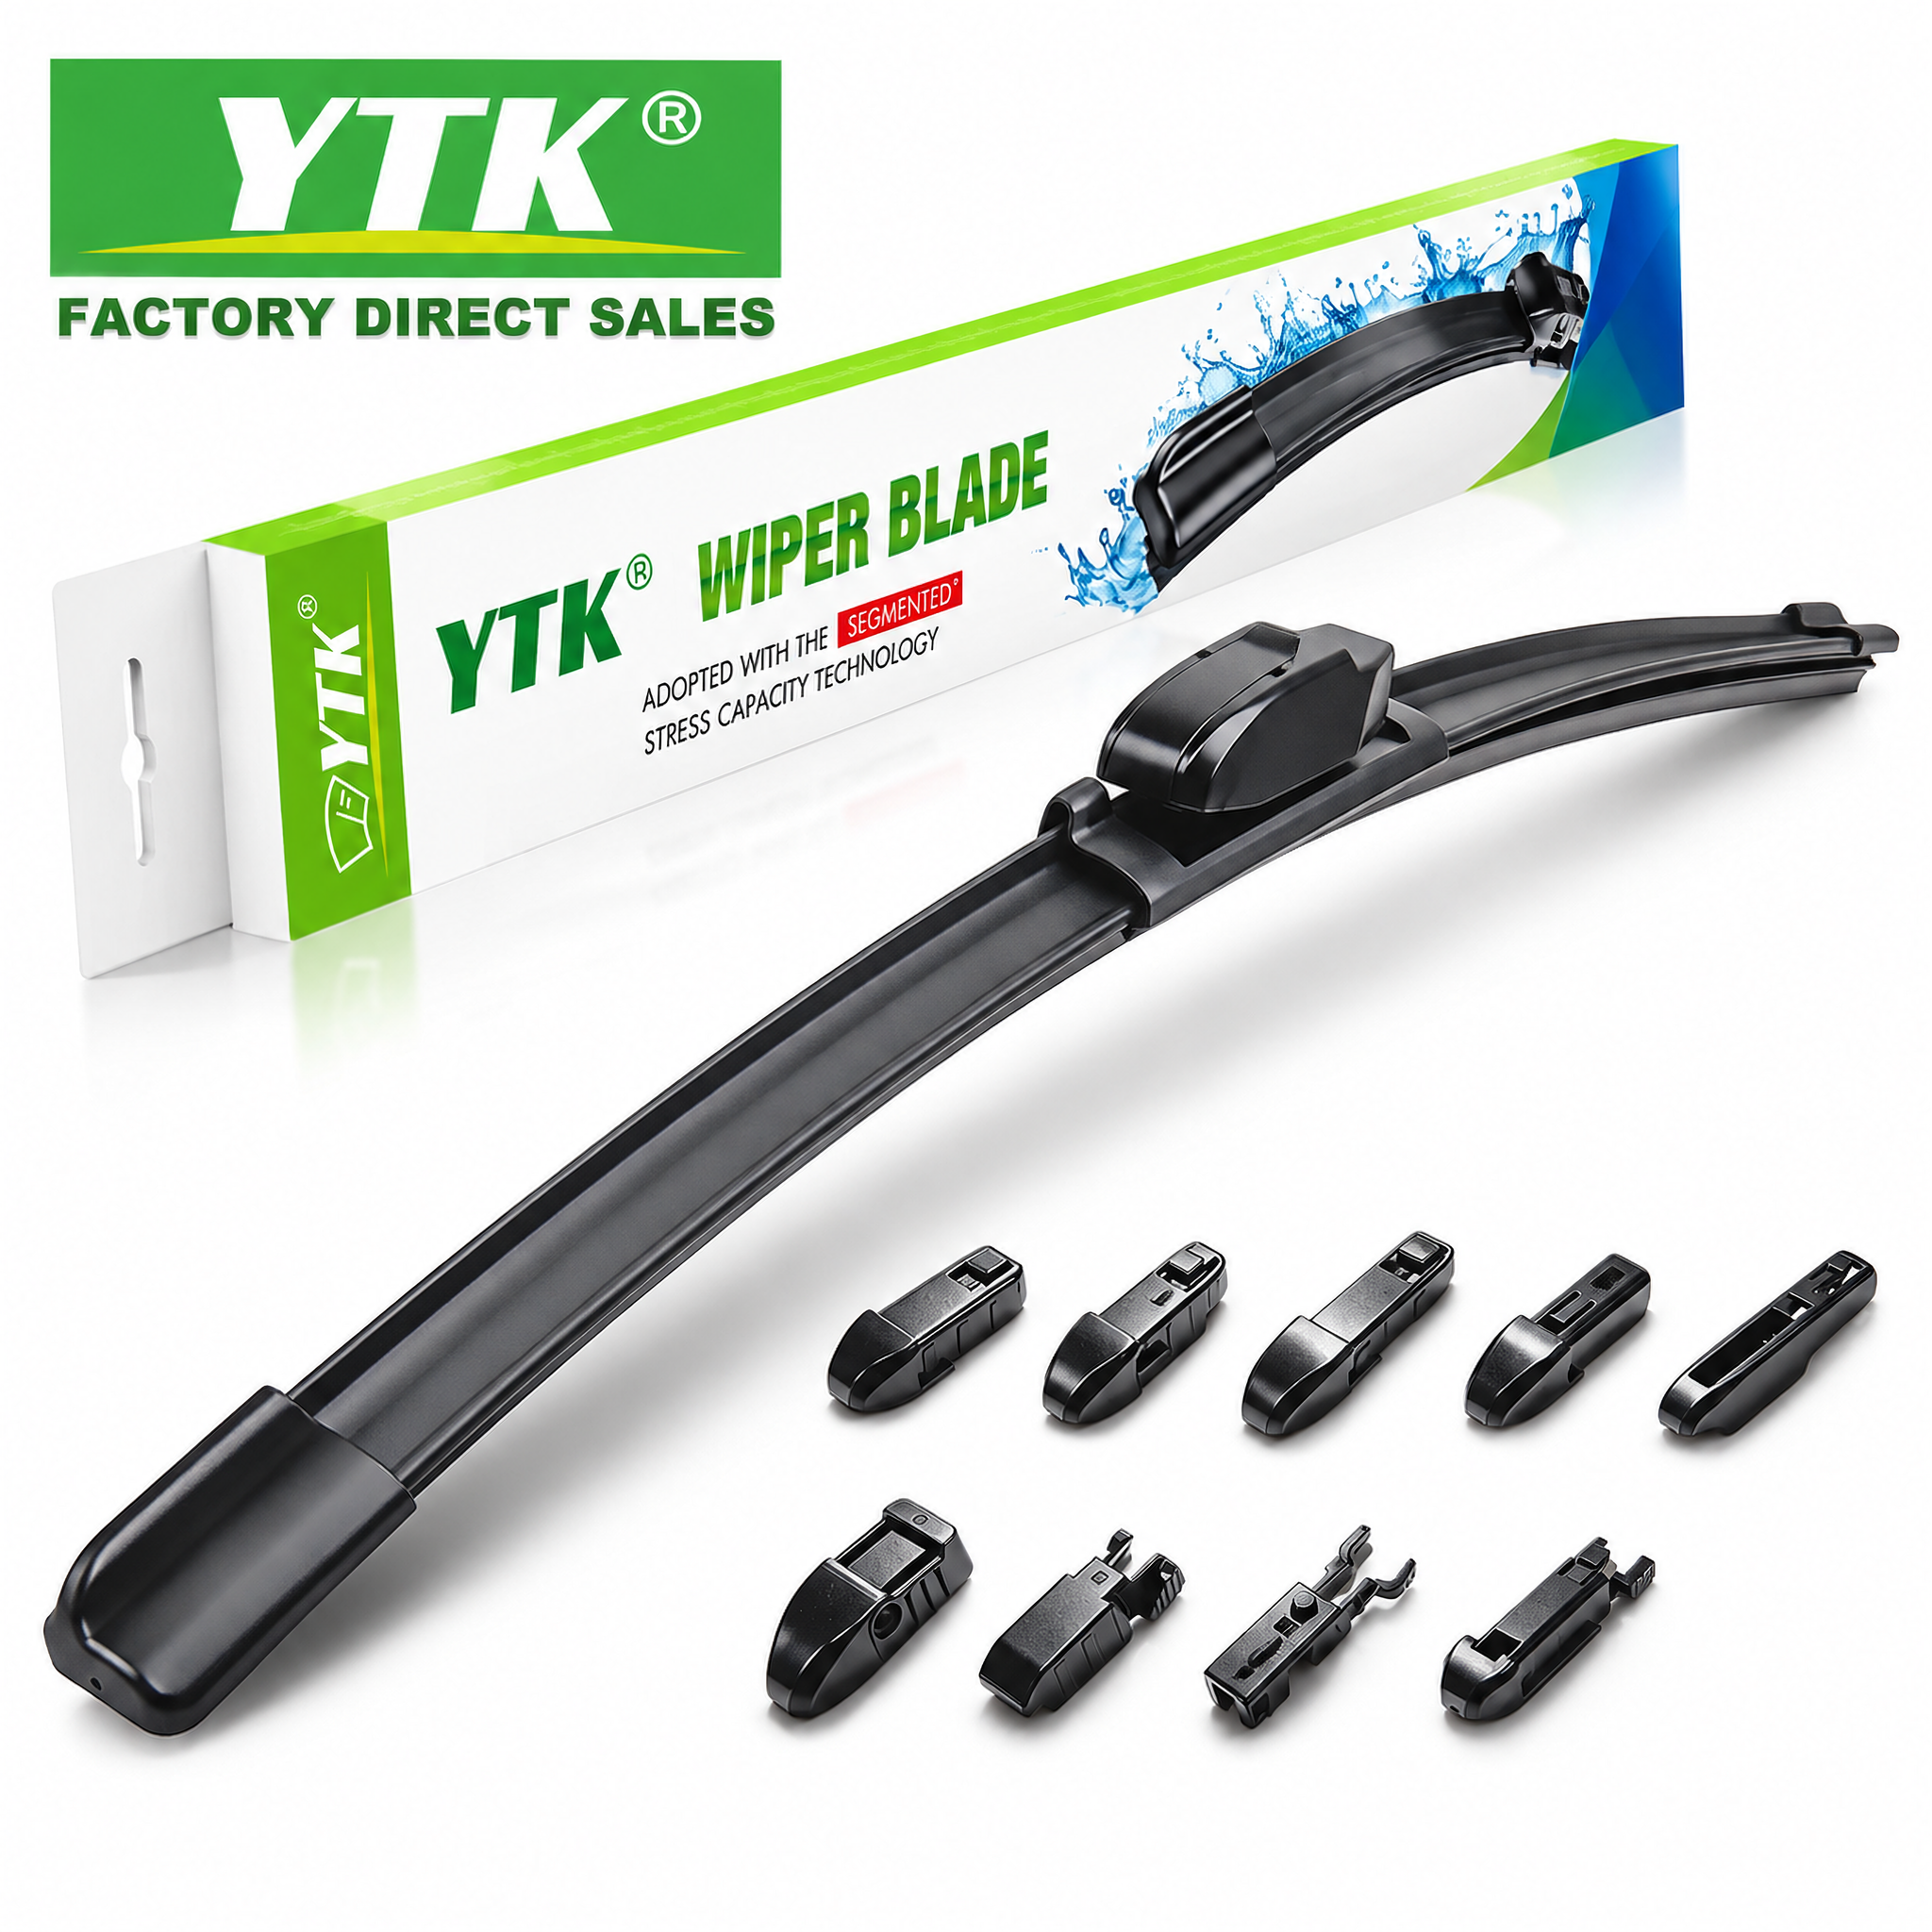
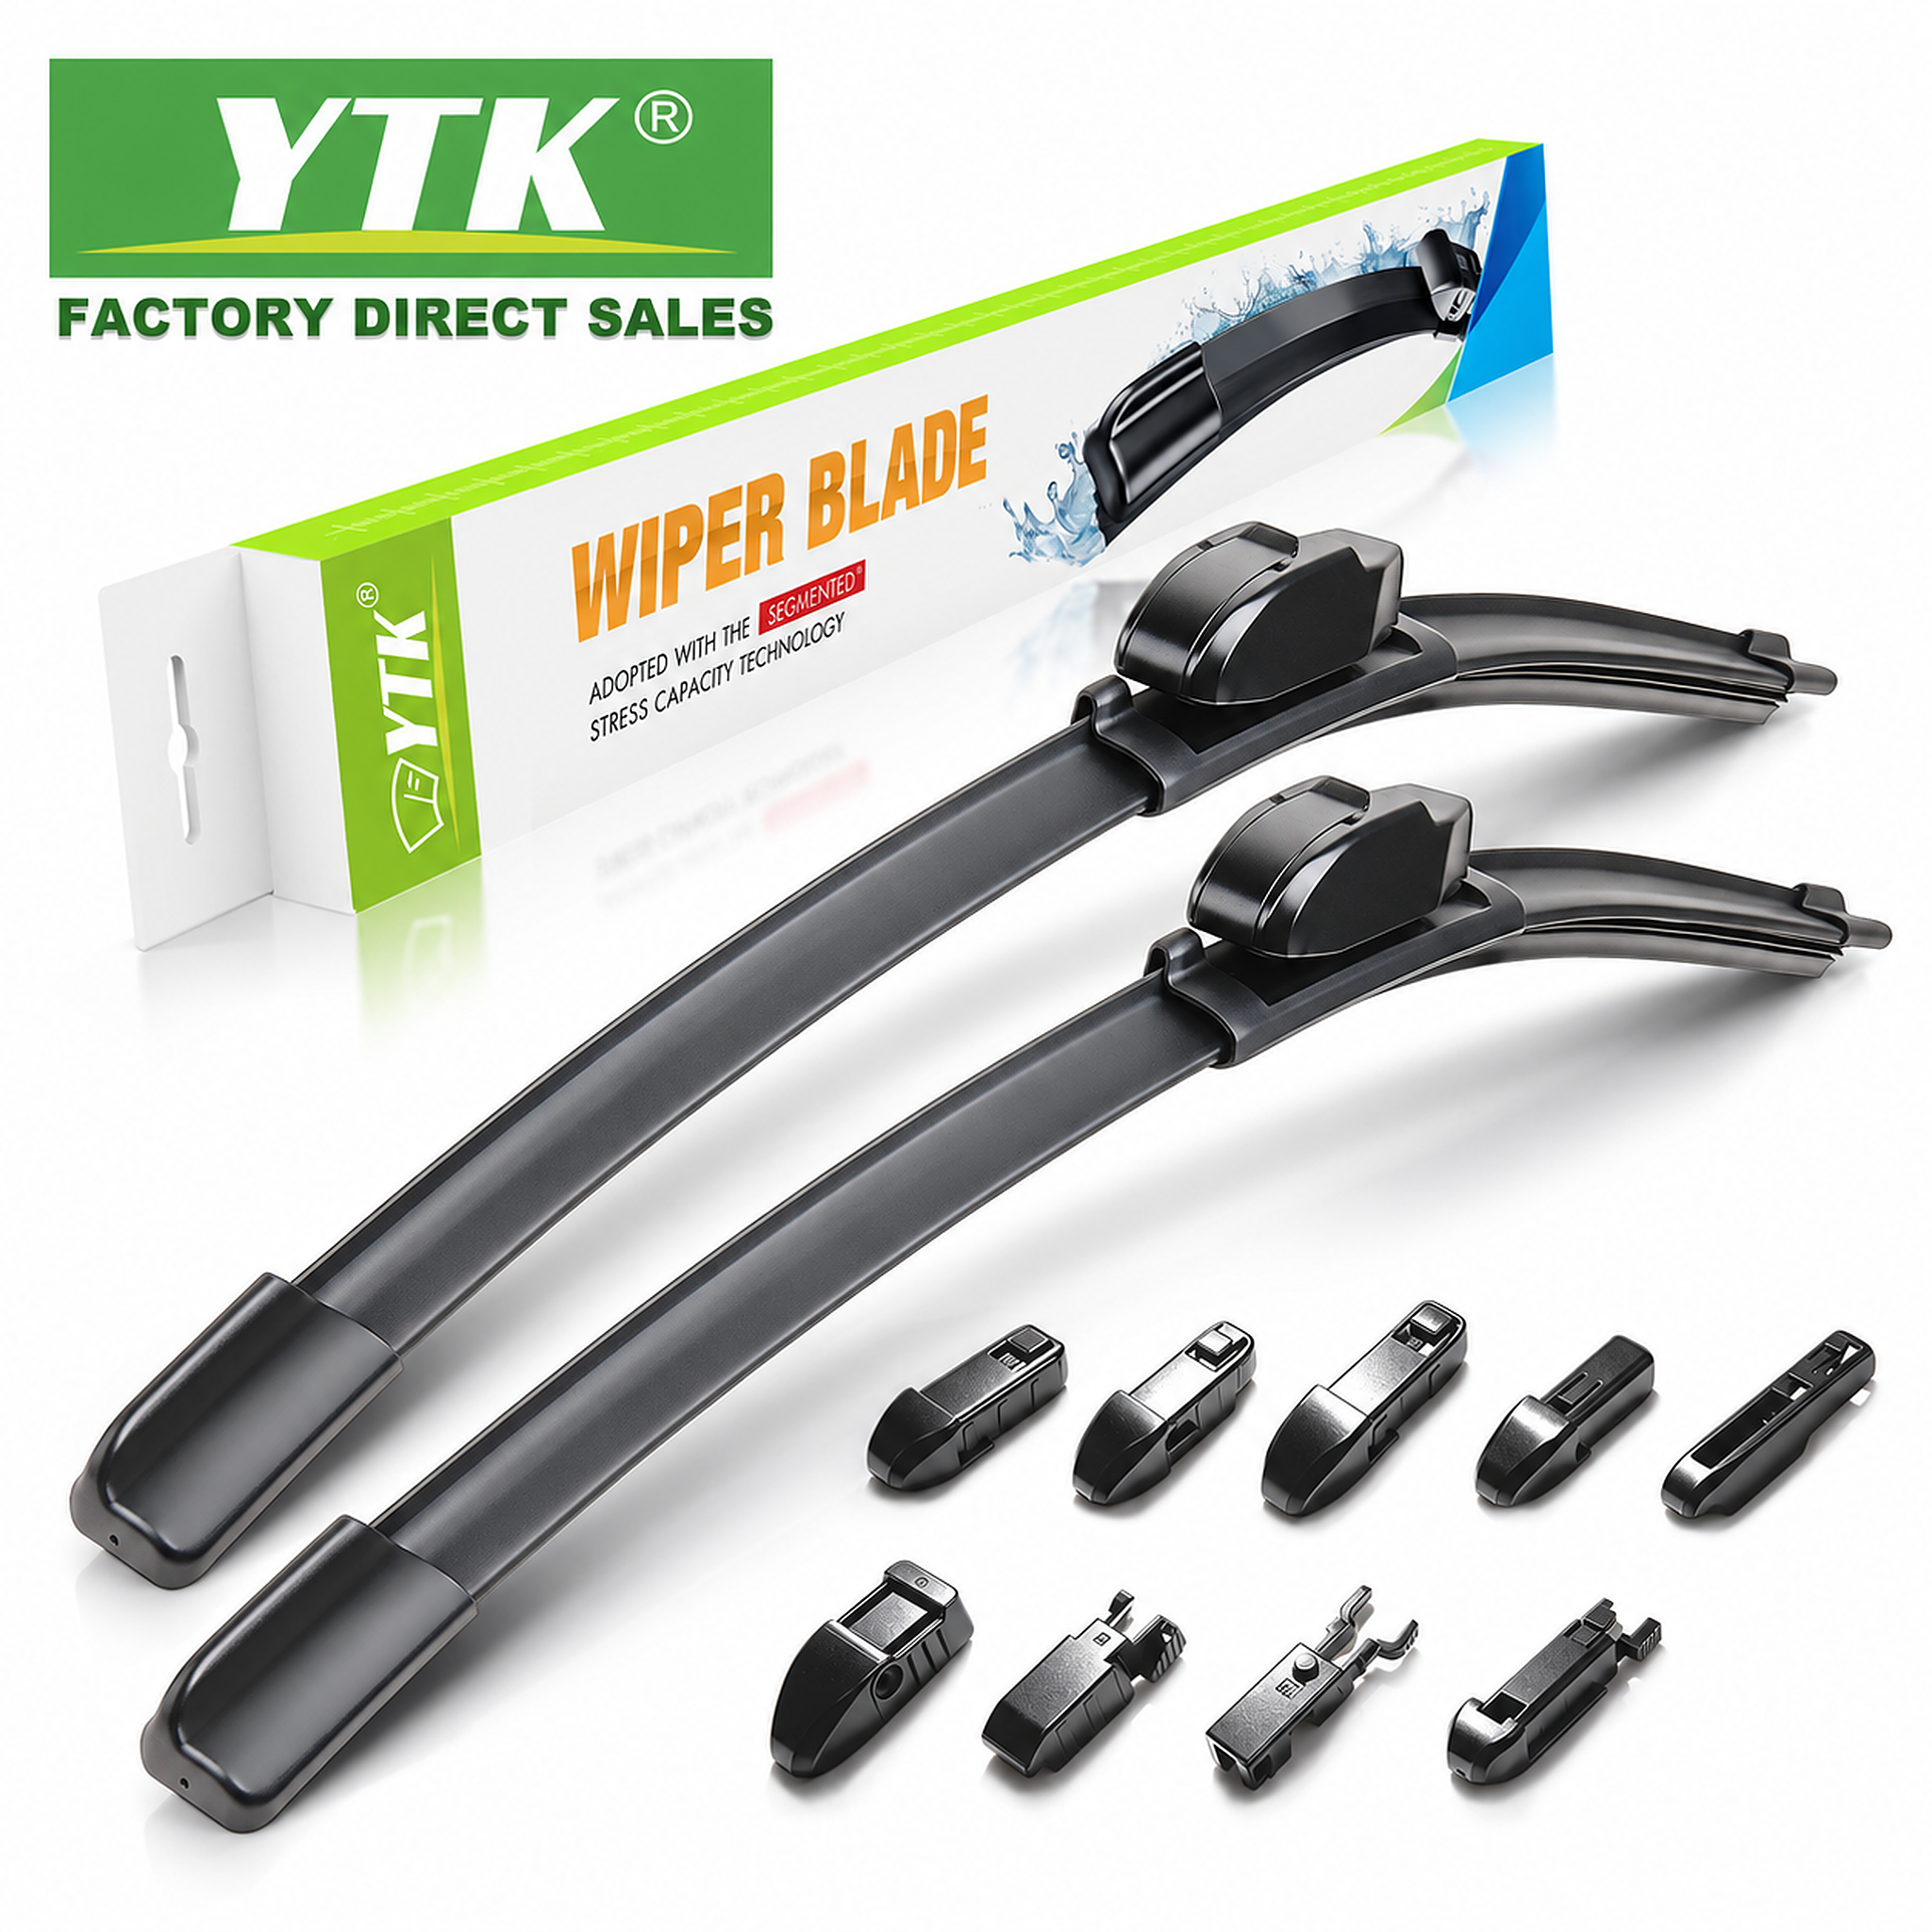
High-integrity driveline center support bearings, precision universal adapters, boneless wiper blades, and winter equipment designed to withstand severe torsional deflection and abrasive operating environments.
Industry Whitepaper: Strategic Procurement of Truck Center Support Bearings
Commercial vehicle driveshaft architectures depend on intermediate center support bearings (commonly designated as carrier bearings or propshaft supports) to sustain multi-piece driveline equilibrium. In heavy-duty logistics, off-highway transport, and light commercial vehicles, driveline center support bearings bear substantial radial shock loads while isolating chassis structural components from high-frequency torsional vibration. Sourcing these mission-critical components directly from specialized Chinese manufacturing hubs demands an integrated understanding of metallurgical durability, elastomer dampening hysteresis, and dynamic sealing integrity.
Since founding operations in Taojiatun Industrial Park, Xingtai, in 1997, our facility has maintained deep engineering competency in both dynamic friction management and elastomeric formulation. Originally founded on heavy-vehicle chassis hardware and center support bearing assemblies, our continuous investment has scaled into automated steel forming, precision cold stamping, and vulcanized rubber bonding. When international distributors, tier-one replacement brands, and fleet operations partner with our Hebei production base, they leverage direct access to an annual production value of US$50M–US$100M with verified factory-floor batch traceability.
Precision Deep-Groove Core
Bearings feature 100% GCr15 high-carbon chromium bearing steel races ground to ABEC-3 (ISO Class 6) tolerances. Controlled raceway micro-geometry prevents micro-spalling under heavy cyclic torque reversal.
Elastomeric Cushion Dampening
Our proprietary synthetic EPDM and natural rubber compounds undergo computerized rheological compounding to ensure consistent durometer rating (Shore A 55–65) across extreme temperatures (-45°C to +125°C).
Multi-Lip Labyrinth Sealing
Equipped with dual-barrier contact nitrilation seals backed by cold-rolled stamped steel deflectors, effectively preventing premature failure caused by slurry, road salt, moisture, and abrasive sand infiltration.
Driveline Engineering Evolution & Future Market Trends
The commercial transport ecosystem is witnessing a significant shift driven by higher freight loading densities, longer cross-country haulage cycles, and rapid fleet hybridization. Driveline components must now support greater peak starting torques while minimizing unsprung chassis weight and parasitic rotational drag. Engineering research within our Nangong and Xingtai workshops has centered on tackling these precise operational bottlenecks:
Higher Torsional Resiliency
As electric and hybrid commercial powertrains deploy immediate maximum torque, carrier rubber isolators must prevent premature shear failure while attenuating higher-frequency driveline oscillations.
Eco-Friendly Compound Formulations
Aligning with REACH and global SVHC guidelines, our rubber compounding lines eliminate harmful plasticizers and PAH compounds while maximizing ozone resistance and long-term elasticity retention.
Modular Bracket Architecture
Modern fleet managers prefer multi-application structural frames that allow standardized core bearing cartridges to fit diverse commercial chassis configurations, simplifying inventory carrying costs.
B2B Purchasing Trends: What Importers Look for in 2026–2030
Professional automotive aftermarket buyers have pivoted from fragmented spot-purchasing toward comprehensive supply chain consolidation. In today’s competitive distribution landscape, sourcing success is determined by five primary procurement parameters:
1. Direct Factory Transparency vs. Intermediary Markups: B2B volume distributors are auditing supplier footprints directly. With verified TÜV Rheinland on-site factory assessments and documented production facilities, JES eliminates broker markups while assuring uncompromised metallurgical standards across every batch.
2. Mixed-SKU Full Container Consolidation: Managing working capital requires flexible shipment configurations. Our operations allow global distributors to combine heavy-duty center support bearings with universal flat wiper blades, multi-adapter assemblies, silicone replacements, and seasonal winter maintenance tools in combined 20GP or 40HQ containers.
3. Rigorous Life-Cycle Validation Data: Quality managers demand accelerated salt spray testing (exceeding 240 hours without white rust on brackets), dynamic balancing compliance, and continuous radial load fatigue analysis to minimize expensive warranty claims in demanding operating environments.
Enterprise Advantages: Why Partner With Us
Over two decades of precision manufacturing excellence backed by verified international quality management systems.
Fully Integrated Production
Over 30,000 m² of plant space operating 10+ dedicated lines, covering stamping, rubber vulcanization, precision bearing assembly, and custom retail packaging.
TÜV Rheinland Assessed
Our manufacturing base has undergone rigorous on-site supplier verification by TÜV Rheinland, providing complete transparency into legal compliance and production integrity.
60+ Export Destinations
Serving aftermarket leaders across North America, Western Europe, Northern Europe, Latin America, Southeast Asia, and Australia under FOB, CFR, and CIF trade terms.
Comprehensive OEM/ODM Service
Turnkey private label branding, custom bracket engineering, bespoke laser etching, barcoded packaging, and private label carton palletizing ready for logistics fulfillment.
Frequently Asked Questions by Professional Buyers
Direct technical and operational answers to streamline your vendor evaluation and procurement process.
Ready to Enhance Your Driveline & Wiper Program?
Connect with our technical engineering and export teams today. Receive comprehensive technical drawings, interchange cross-reference lists, and our complete wholesale product catalog.
Get Catalog