Featured Product Series & Factory Assemblies
Verified automotive commercial replacements, universal systems, and private-label production lines engineered for global aftermarket distributors and Tier-1 procurement networks.
Precision Heavy-Duty V Rod Bushings: Structural Mechanics, Elastomeric Compounds & Manufacturing Integrity
In modern commercial vehicles, the suspension torque rod system and its central V-stay (or V-rod) withstand massive longitudinal braking forces, transverse cornering reactions, and multidirectional axle articulation. Sourcing V-rod bushings requires strict validation of mechanical metallurgy, dynamic fatigue limits, and elastomeric-to-metal chemical vulcanization.
As a leading Chinese manufacturer and supplier of heavy-duty suspension bushings, center support bearings, and high-performance rubber-metal automotive components, Xingtai JES Auto Parts Manufactuer Co., Ltd. produces industrial-grade V-rod bushings for European, North American, and Asian commercial vehicle chassis platforms. Whether stabilizing heavy trucks from Mercedes-Benz (Actros), Volvo (FH/FM), Scania, MAN, and DAF, or regional haulers like Sinotruk HOWO and Shacman, our factory ensures exact dimensional tolerances, high durometer resilience, and extended service life.
The primary failure mode of secondary aftermarket torque rod bushings is vulcanization delamination: under continuous shear and high ambient temperature, the rubber core pulls away from the steel inner sleeve, causing uncontrolled axle movement, premature tire wear, and critical steering instability. JES Auto Parts mitigates this through automated multi-stage degreasing, shot-blasting, robotic Chemlok® adhesive application, and temperature-controlled compression molding vulcanization.
| Bush Series / Fitment | Outer Diameter (mm) | Inner Pin Hole (mm) | Bolt Hole Center (mm) | Hardness (Shore A) | Tensile Strength (≥ MPa) | Elongation (≥ %) | Typical OEM Cross |
|---|---|---|---|---|---|---|---|
| JES-VRB-01 (Volvo Series) | Ø 85 mm | Ø 25 mm | 152 mm | 75 ± 5 | 18.5 MPa | 450% | 20741758 / 20374154 |
| JES-VRB-02 (Mercedes Actros) | Ø 95 mm | Ø 28 mm | 130 mm | 78 ± 5 | 19.0 MPa | 420% | 000 350 4205 / 000 350 5605 |
| JES-VRB-03 (Scania 4/P/G/R) | Ø 75 mm | Ø 21 mm | 115 mm | 72 ± 5 | 17.5 MPa | 480% | 1379743 / 1387283 |
| JES-VRB-04 (MAN TGA/TGX) | Ø 85 mm | Ø 24 mm | 130 mm | 75 ± 5 | 18.0 MPa | 460% | 81.43230.6053 / 81.43230.6054 |
| JES-VRB-05 (Renault/DAF) | Ø 90 mm | Ø 26 mm | 140 mm | 76 ± 5 | 18.2 MPa | 440% | 5010 294 147 / 1320875 |
| JES-VRB-06 (Mining & Severe Haul) | Ø 108 mm | Ø 32 mm | 168 mm | 82 ± 5 | 21.0 MPa | 400% | AZ9725529272 / Heavy Heavy Duty |
V-Stay & Suspension Torque Rod Bushing Product Categories
Engineered for high load stability, vibration isolation, and exact OEM replacement across various regional fleet profiles.
Solid-Core Cylindrical Bushings
Constructed with cold-drawn seamless carbon steel outer shells and high-density vulcanized natural rubber (NR) compounded with premium polybutadiene. Optimized for high radial load containment in long-haul highway line trailers and 6x4 tractor units where minimal deflection and steady axle alignment are vital.
Dual-Pin Tapered V-Rod Bushings
Engineered with drop-forged 40Cr/42CrMo central steel pins featuring integrated mounting holes. This design facilitates bolt-on installation into casting brackets. Precision heat-treatment (quenching and tempering to 28-32 HRC) guarantees yield strength under extreme braking torque spikes.
Extreme Severe-Duty Polyurethane Range
Formulated with castable MDI-based polyurethane elastomer systems for off-highway mining tippers, logging transports, and industrial construction vehicles. Yields superior resistance to oil, rock gouging, abrasion, and aggressive hydrolytic wash-down environments with Shore hardness up to 90A.
Segmented Deflection Torque Bushings
Designed with engineered elastomer voids along the non-load axis to deliver tuned asymmetric stiffness. These bushings allow smooth angular articulation during severe chassis twisting over uneven logging roads while maintaining high longitudinal rigidity for braking stability.
Complete V-Stay Rod Assemblies
Factory-assembled, balanced, and press-fitted V-arms combining robotic welding of thick-wall tubular bodies with precision cold-pressed bushings. Shipped ready-to-mount for fleet maintenance depots, eliminating the need for high-tonnage workshop hydraulic pressing equipment.
Custom OEM Private-Label Bushings
Dedicated tooling, custom durometer compounding, laser engraving of customer trademarks, and color-coded corrosion-resistant coatings. Full packaging customization—from anti-corrosion VCI sealed polybags to heavy-gauge distributor carton packaging with barcodes.
Future Purchasing Trends for Commercial Vehicle Suspension Bushings
How Tier-1 buyers, wholesale distributors, and global fleet fleets are optimizing total cost of ownership (TCO) and mitigating supply-chain vulnerabilities.
The global commercial vehicle suspension components market is experiencing fundamental structural transitions. Procurement directors are no longer evaluating suppliers based solely on initial FOB unit price. Instead, multi-dimensional total cost of ownership (TCO), material sustainability, and digital traceability are defining procurement decisions across North American and European logistics corridors.
1. Shift Toward Direct Factory Sourcing & Intermediary Elimination: Leading aftermarket brands and regional parts cooperatives are systematically bypassing domestic trading houses to establish direct engineering partnerships with verified Chinese manufacturing facilities like Xingtai JES Auto Parts. By collaborating directly with the vulcanization factory, procurement teams save 18% to 32% on landed costs while gaining direct access to production PPAP documentation, mill test certificates (MTC), and customizable elastomer formulations.
2. Higher Demands from Commercial EV Trucks: Heavy battery-electric commercial trucks (such as Class 8 haulers and 40-ton European electric tractors) present drastically increased curb weights and deliver instantaneous, full-torque acceleration. Conventional rubber bushings experience accelerated fatigue and premature shear failure in these duty cycles. As a result, forward-looking buyers are stocking High-Damping High-Tensile (HDHT) hybrid bushings engineered to withstand 35% higher torsional loads without increased permanent set.
3. Supply Chain Nearshoring vs. Resilient Chinese Production Hubs: While regional nearshoring has gained traction, China's concentrated supply chain—integrating upstream steel tube mills, synthetic and natural rubber processing, automated mold making, and advanced electroplating—ensures unmatched cost efficiency, scale, and delivery speeds. Leading global buyers are managing geopolitical risk by signing multi-year framework supply agreements with certified Chinese manufacturers possessing verified export track records.
Technological Developments in Rubber-to-Metal Vulcanization
Microstructure optimization, molecular bonding chemistries, and automated compression molding driving the next generation of suspension life.
Nano-Carbon Dispersion & Anti-Ozone Blends
By integrating furnace-grade carbon black at nano-scale dispersion levels along with microcrystalline paraffin waxes and p-phenylenediamine (6PPD) antioxidants, JES elastomer compounds resist environmental ozone attack, dynamic thermal buildup, and oil spray, avoiding the surface cracking typical in standard commercial bushings.
Automated Chem-Lock® Primer Activation
Our facility has replaced manual dipping with robotic dual-spray Chemlok® adhesive systems. Steel cores and outer shells are heated to 65°C prior to primer and adhesive application, creating a cross-linked chemical covalent bond during vulcanization that withstands inter-laminar shear stresses exceeding 25 MPa.
Nonlinear FEA Stress Distribution Optimization
Using advanced Finite Element Analysis (FEA), our chassis engineers model axial, radial, and cardanic angular deflections before metal tooling begins. Optimizing internal contour radii reduces localized peak stress concentrations by 42%, virtually eliminating internal tear initiation under severe vehicle impact loads.
Xingtai JES Auto Parts: 25+ Years of Manufacturing Leadership
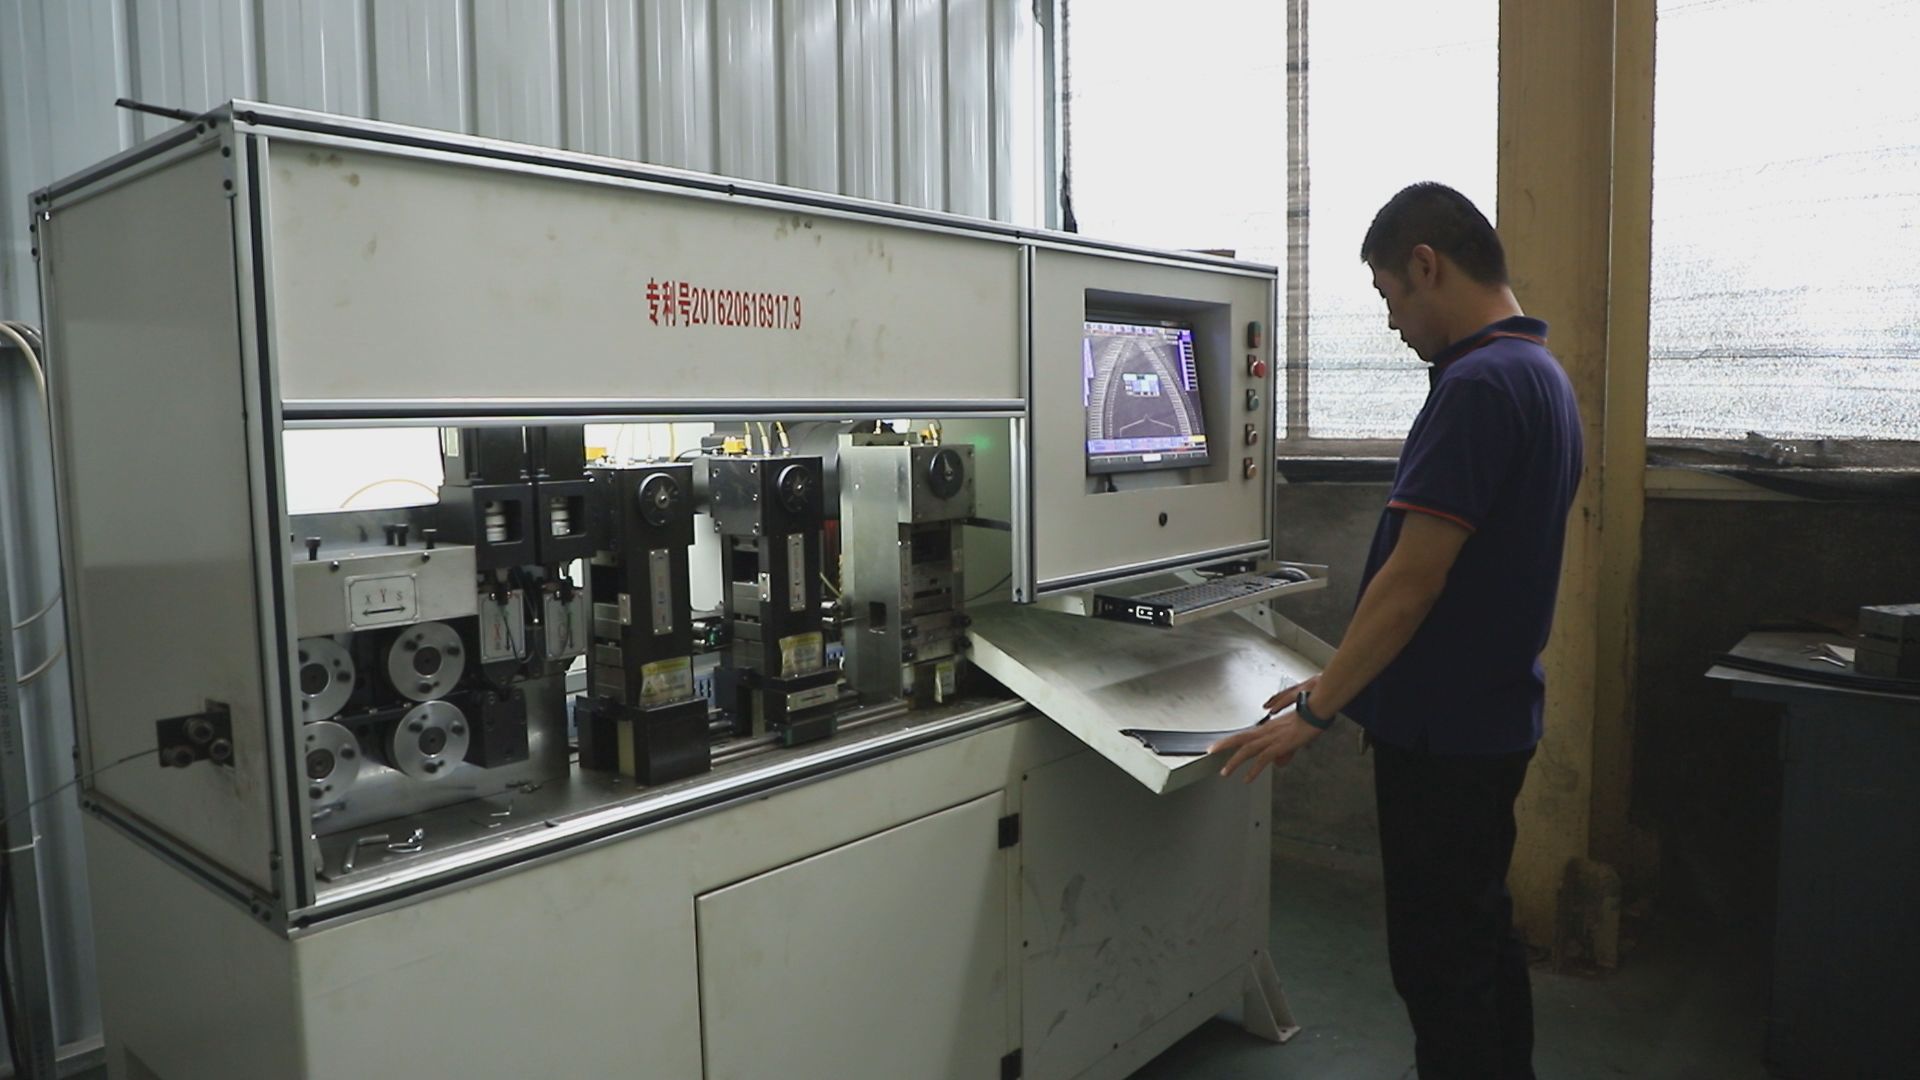
Founded in 1997, Xingtai JES Auto Parts Manufactuer Co., Ltd. has grown from an engineering workshop specializing in drivetrain center support bearings and heavy-duty chassis components into a 30,000 m² modern manufacturing enterprise. Based in Taojiatun Industrial Park, Hebei Province, our vertically integrated plant houses 10+ automated production lines, a dedicated rubber mixing facility, and an advanced metallurgical laboratory.
Holding on-site verified supplier status certified by TÜV Rheinland and operating in accordance with automotive IATF 16949 quality practices, JES delivers high manufacturing consistency for large-volume importers, regional brand owners, and Tier-1 automotive groups globally.
Frequently Asked Questions: Sourcing V Rod Bushings from China
Actionable answers to technical, commercial, and operational questions asked by wholesale importers, procurement managers, and fleet parts buyers.
What is the standard MOQ for wholesale and custom-branded V rod bushings? +
How does your factory prevent rubber-to-metal vulcanization bonding failure? +
What steel grades and heat treatment procedures are used for the central pin and outer shell? +
Can you provide customized durometer hardness for extreme cold or hot mining climates? +
What quality testing documentation accompanies container shipments? +
What are your international trade, payment terms, and typical production lead times? +
Direct Factory Partnership: Request a Sourcing Quotation
Eliminate middleman markups and secure reliable, heavy-duty suspension parts directly from our Hebei production base. Share your OEM part numbers, technical drawings, or volume requirements for a comprehensive factory price analysis within 24 hours.
- IATF 16949 & TÜV Verified Production Standards
- Rapid 48-Hour Technical Feasibility Review
- High-Capacity Logistics via Tianjin & Qingdao Seaports
- Dedicated English, Spanish & Russian Export Support
